
 202 Products in 18 Families
 Packaging Built Around the Buyer
 From Brief to Approved Sample
 Cosmetic Packaging Buyer Guide
Catalog labels are a poor shortcut for this decision. A conventional lotion pump generally uses a dip tube and a familiar repeated stroke. “Treatment pump” often describes a smaller or more controlled dispensing interaction, but suppliers use the term differently. An airless package changes the evacuation architecture, commonly through a moving piston or collapsible inner system. Those labels describe starting points; project samples still have to establish how the formula and package behave together.
A workable shortlist answers five questions first: How does the formula flow and recover after shear? What dose and application pattern does the user need? How will residual product be measured? How will the package be filled and assembled? Which tests represent its expected life? Once those constraints are visible, appearance can be compared without masking a functional mismatch.
The three systems solve different jobs
| Decision dimension | Conventional lotion pump | Treatment pump | Airless system |
|---|---|---|---|
| Typical buyer objective | Convenient repeated dispensing from a dip-tube bottle | Controlled presentation and a smaller or focused dispensing interaction | Evacuation without a conventional dip tube and controlled delivery as internal volume changes |
| Formula route | Product travels through dip tube and pump chamber | Usually a dip-tube or compact pump path, depending on design | Product is displaced by piston, pouch, or other airless architecture |
| Main specification focus | Neck fit, tube length, output, lock, actuator, pack height | Dose, actuator feel, orifice, closure fit, premium component stack | Complete package geometry, priming, piston/pouch movement, venting design, fill and assembly route |
| Common project risk | Tube reach, prime loss, leakage, actuator loads in shipment | Definition varies across suppliers; appearance can obscure output and formula limits | “Airless” label can hide different mechanisms; filling and residual behavior are system-specific |
| Approval evidence | Assembly, output, prime, compatibility, leakage, distribution | Same core evidence plus precise dose/user-interface review | Priming, dose consistency, evacuation/residual assessment, compatibility, storage and distribution in final system |
This comparison is intentionally qualitative. There is no universal viscosity cut-off, output number, or residual-rate threshold that makes one architecture correct. Suppliers test with different liquids, methods, conditioning, and sample configurations. A number copied from one catalog should not be used as a neutral boundary for all products.
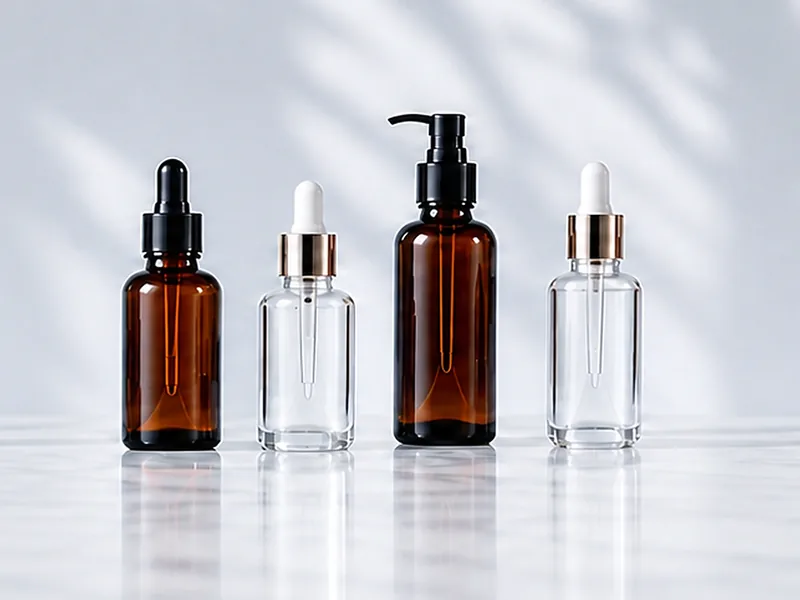
Conventional lotion pumps: flexible, familiar, but still a system
The conventional pump-and-dip-tube format is familiar to fillers and consumers. It can support many bottle capacities, closure finishes, actuator designs, locks, colors, and decoration routes. This flexibility is valuable when the project needs a recognizable dispensing gesture, a larger actuator surface, or a bottle format that can be sourced and decorated separately from the pump.
Its apparent simplicity can cause weak specifications. Tube length is sometimes treated as an afterthought; output is accepted from a catalog; the bottle and pump are purchased from separate sources without a controlled mating review; or the filled pack is shipped with an actuator that receives carton load. Each of those shortcuts turns a flexible architecture into a variable one.
A lotion-pump shortlist should therefore begin with the bottle neck and the formula path. Ask what internal components contact the product. Check whether the formula can prime the selected chamber, return after actuation, and continue dispensing as the bottle empties. Evaluate the tube’s position when the bottle is upright and tilted, and define whether the user will turn, clip, or cap the actuator between uses. If the product is sold through parcel delivery, review the locked pump as part of the carton pack-out rather than as an isolated closure.
This architecture can be appropriate when the formula and desired dose work with the pump design, the filler can apply the closure consistently, and the brand accepts the residual behavior of a dip-tube bottle. It is not automatically inferior to airless, nor is it automatically suitable for every lotion.
Treatment pumps: first define what the supplier means
“Treatment pump” is the most ambiguous term in this comparison. It often describes a compact, premium, or lower-output dispenser intended for facial-care or targeted-use products. But it can refer to different chamber constructions, closure sizes, actuator shapes, and dose ranges. The first procurement task is therefore definitional: obtain the drawing, component description, nominal output test basis, and compatible bottle or closure family.
Treatment-pump projects often place greater weight on dose perception and user control. A small change in actuator travel, spring force, orifice geometry, or output can be noticeable when the product is applied to a limited area. The brand may also expect a more refined collar, overcap, or metal-look finish. Those aesthetic layers create extra interfaces that require review: cap retention, collar movement, scuffing, color alignment, dimensional stack-up, and the effect of decoration on assembly.
Do not infer that a treatment pump is more “precise” simply because it is smaller. Precision requires a defined method and repeatable results under relevant conditions. The buyer should decide whether the important measure is average dose, variation between strokes, variation between units, initial prime behavior, force, stream shape, or user-perceived control. The sample plan then measures those attributes with the project liquid or a justified surrogate before final formula work.
A treatment pump is a reasonable candidate when the intended interaction is controlled and the supplier can document the exact configuration. It should not be used as a marketing synonym that bypasses technical comparison.
Airless systems: architecture changes the project
Airless packaging is not a single pump placed on a standard bottle. It is a family of systems designed to dispense as internal volume changes, often through a piston that moves upward or an inner pouch that contracts. Designs differ in venting, piston sealing, pump chamber, base construction, filling access, assembly sequence, and refill or non-refill intent. Those differences affect how the pack is filled, primed, stored, tested, and recycled or disassembled.
The absence of a conventional dip tube can support a clean visual presentation and different evacuation behavior. It may also reduce the way outside air is exchanged through the package during use, depending on the system. That observation must not be converted into a blanket preservation claim. Formula protection depends on the complete package, component materials, permeation, seal performance, filling, headspace, user handling, and the formula owner’s stability evidence.
Airless systems demand early coordination with the filler. Some packages require bottom filling or a specific piston position; others are top-filled and assembled in a controlled sequence. Trapped air, fill level, product temperature, and assembly can affect priming and evacuation. The filler should review equipment, holding fixtures, cleaning, filling nozzle, fill speed, package support, and closure application before the design is locked.
Approval should include priming, output consistency, actuation, residual product, leakage, compatibility, storage orientation, and distribution evaluation. A sample that dispenses a few times on a desk does not establish life-cycle performance. Neither does a supplier’s generic “airless” declaration.
Formula behavior should be described, not reduced to one viscosity number
Viscosity is important, but a single value can be misleading when the formula is non-Newtonian, thixotropic, temperature-sensitive, aerated, particulate, or changes during storage. Ask the formula team for the measurement method, temperature, shear conditions, range across development batches, and any known packaging sensitivities. If those data are not yet final, state that the package shortlist is provisional.
Other useful inputs include density, surface behavior, oil or solvent concerns, pH where relevant to material review, particles or suspended actives, fragrance load, foaming tendency, and sensitivity to shear. Confidentiality may limit disclosure, but the parties can still identify risk categories and agree on who receives the full formula information.
The buyer should also describe recovery between uses. A product can move through the pump during a rapid bench test but fail to refill the chamber after standing, or behave differently at low temperature. Conversely, a low-viscosity formula may reveal leakage paths that a thick surrogate does not. The sample matrix should represent intended storage and use, not only a convenient room-temperature demonstration.
Dose is a consumer-use requirement and a test definition
Start from how the product is applied. Does one complete stroke represent one use, or will the consumer use several strokes? Is partial actuation expected? Is the dose applied to a fingertip, cotton pad, broad skin area, hair, or another surface? Is a stream, ribbon, controlled bead, or soft deposit desired? These questions translate marketing language into observable dispensing behavior.
Then define how dose will be measured. Specify priming, conditioning, stroke speed and travel, sample quantity, discarded initial strokes, number of measured strokes, units, liquid, and statistical summary. If output is converted between mass and volume, record density and method. If partial strokes matter, test them deliberately rather than assuming a full-stroke result predicts them.
ASTM’s F02.30 mechanical-dispenser committee lists active practices for output per stroke, priming strokes, actuation force, functional stability, and other pump characteristics. The official index is a useful method map, but the full current standard and a project-specific protocol are needed for formal testing. A standard title should never be used as decoration in an RFQ.
Evacuation and residual product: compare like with like
Residual-product discussions often become marketing claims because the denominator, endpoint, and test setup are not stated. A buyer should define the initial filled mass, net product mass, priming treatment, actuation method, package orientation, endpoint, conditioning, and how product on internal surfaces is handled. Decide whether the result is reported as mass, percentage, or another measure. Record packages that stop dispensing for a functional reason rather than forcing a numerical average to hide failures.
Conventional bottles and airless systems may need different handling, but the buyer’s decision question should remain consistent: how much of the intended fill can the user dispense under the defined use simulation, and what failure modes appear? A favorable result with one formula and fill process is not a universal package claim. Repeating the method after a component, formula, or filling change may be necessary.
Residual performance is only one selection criterion. A format with lower measured residue may introduce filling complexity, higher component count, a different recycling route, or decoration limits. The comparison should preserve those trade-offs.
Filling and assembly can eliminate an otherwise attractive option
Before requesting decorated samples, map the filling route for each candidate. Identify component delivery state, incoming inspection, bottle or airless-body support, filling direction, nozzle clearance, fill-temperature restrictions provided by the formula/process owner, headspace or piston position, pump insertion, closure application, lock state, coding, and secondary packing.
Ask the filler to review actual drawings and samples. A line that handles threaded lotion pumps may not handle a particular airless body without change parts. A compact treatment pump may create cap-placement or torque-control challenges. Manual pilot filling can conceal issues that become important at production speed. The project should record whether a sample was manually assembled, run on pilot equipment, or verified on the intended line.
No article can supply a generic production speed or setup time. Those depend on equipment, package geometry, component presentation, formula, cleaning, quality plan, and operator controls. The comparison should instead produce a list of line-trial questions and responsible owners.
A buyer’s shortlist matrix
Score candidates only after defining “evidence available” separately from “expected benefit.” A simple matrix can use four states: demonstrated under project conditions, supported by relevant supplier data but not project-tested, unknown/TBC, and does not meet requirement. This is more honest than a numeric score that treats assumptions as facts.
Consider these rows:
- formula path and contact-material information;
- bottle/closure or complete-system dimensional control;
- target dose and measured consistency;
- prime and re-prime behavior;
- evacuation/residual result under a defined method;
- lock, overcap, and shipment protection;
- filling-line feasibility;
- compatibility and storage plan;
- distribution pack-out and test route;
- decoration and color approval;
- component traceability and change notification;
- documentation, sample identity, and revision control;
- commercial scope, quantities, and timing confirmed for the selected build.
The matrix should not award an airless candidate points merely for being airless, or penalize a conventional pump merely for having a dip tube. It should show which architecture can meet the project’s requirements with the strongest evidence and manageable unknowns.
Common selection mistakes
The first mistake is choosing by appearance and asking engineering to make the formula work later. The second is treating a commercial family name as a specification. The third is comparing supplier output numbers measured with unknown liquids and methods. The fourth is discussing formula compatibility without a full contact-material path or defined test. The fifth is approving an empty-packaging bench sample without involving the filler and distribution pack.
Another mistake is assuming an architecture carries a regulatory conclusion. A package can support a product strategy, but the finished-product responsible party remains accountable for market-specific safety, claims, labeling, and documentation. A supplier’s material or test document has a defined scope; it does not approve the finished cosmetic.
Finally, buyers sometimes create three parallel projects instead of a controlled shortlist. Limit early samples to candidates that answer materially different hypotheses. Record why each exists. When one architecture is selected, close the others or document the conditions under which they remain backups. This prevents artwork, carton, stability, and quotation work from advancing on conflicting configurations.
Decision paths by project situation
Choose a conventional lotion-pump route for further investigation when the user experience calls for familiar repeated dispensing, the bottle/closure system can be controlled, the formula primes and delivers under representative conditions, and the filler and distribution pack can handle the assembly. Choose a treatment-pump route when controlled presentation, compact geometry, or a focused dose interaction is important and the exact supplier definition can be documented. Choose an airless route when its evacuation architecture and presentation address a real product objective and the team can support the complete filling, compatibility, functional, and distribution validation program.
Those are shortlist conditions, not final approvals. A project may test two architectures because the formula or filling route is still evolving. The point is to make the uncertainty explicit and time-box the decision rather than declaring a winner from a catalog page.
Build the sample brief
To compare candidate systems, send the formula category and known handling limits, target dose, bottle or capacity preference, desired user interaction, filling route, and distribution channel. A scoped response should identify candidate architectures, information gaps, and a sample/test sequence. It should not assert universal formula compatibility or preservation performance.
Sources and limits
- ASTM Subcommittee F02.30 on Mechanical Dispensers, reviewed 2026-08-13. The official index identifies current practices relevant to pump output, priming, force, component compatibility, dip tubes, and stability. Obtain current full standards for formal use.
- BeautyContainers guide to choosing airless packaging — owner of airless-specific selection details.
- BeautyContainers compatibility testing guide — owner of final package/formula validation planning.
This comparison is a buyer decision framework, not a formula, regulatory, shelf-life, or performance approval. Exact component specifications and evidence remain project-specific.